
A wire drawing die is one of the most critical tooling components in the wire manufacturing process. Even a small change in die condition can affect wire diameter, surface finish, ovality, dimensional accuracy, production speed, and overall tooling cost.
When a wire drawing die fails prematurely, replacing the die is not always the complete solution. The actual cause may also be related to die selection, wire condition, lubrication, alignment, drawing speed, cooling, cleaning, or the way the die is installed and maintained.
Understanding the reason behind die wear or failure helps manufacturers reduce unplanned stoppages, improve wire quality, and achieve more consistent die life.
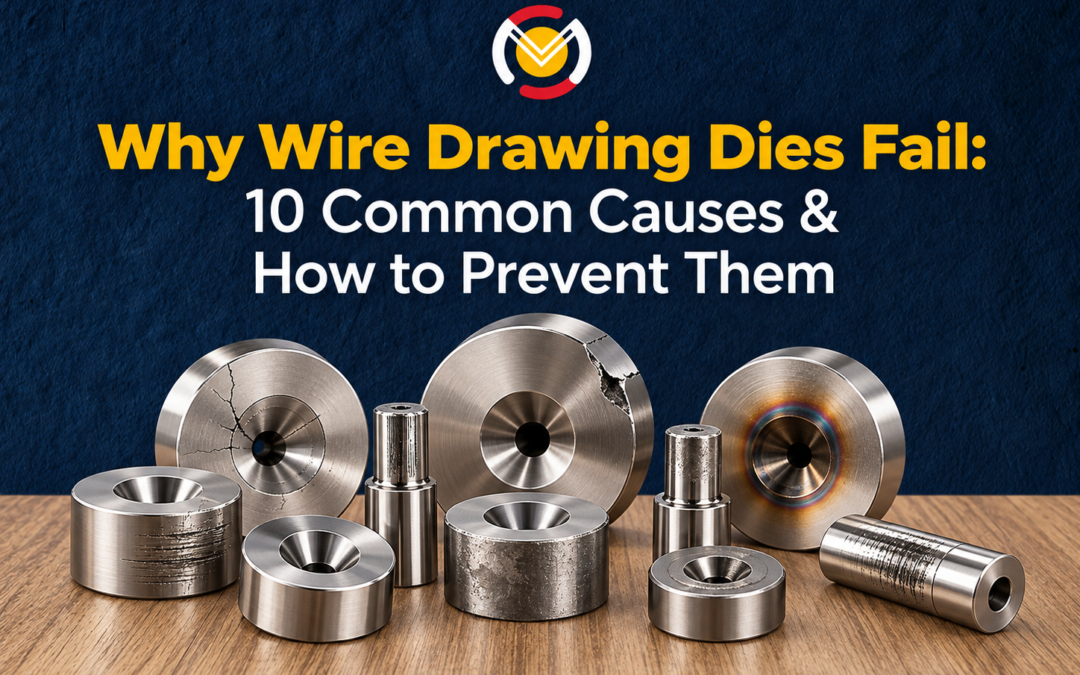
Here are 10 common causes of wire drawing die failure and practical ways to address them.
1. Incorrect Die Material Selection
Different wire materials and drawing conditions require different die materials.
Using a die material that is not suitable for the application can result in accelerated die wear, die cracking, poor surface finish, or unstable dimensions.
For example, tungsten carbide, PCD, natural diamond, and synthetic single-crystal diamond dies have different characteristics and are suited to different operating conditions.
What to Check
- Wire material
- Incoming wire diameter
- Final wire diameter
- Reduction per pass
- Drawing speed
- Required surface finish
- Expected production quantity
- Lubrication conditions
2. Excessive Reduction Per Pass
The amount of reduction taken through a die has a direct effect on the mechanical and thermal load placed on the tooling.
If the reduction is too high for the selected die and drawing process, the die can experience excessive pressure and wear.
This may result in:
- Rapid die wear
- Chipping
- Cracking
- Increased wire temperature
- Poor surface finish
- Dimensional instability
Practical Solution
Review the reduction schedule and ensure that the die is operating within the requirements of the drawing process.
The correct reduction should be considered together with wire material, die geometry, lubrication, and drawing speed.
3. Poor or Inadequate Lubrication
Lubrication is essential for controlling friction and heat during wire drawing.
Insufficient lubrication can increase friction between the wire and die, causing excessive temperature and accelerated die wear.
Typical Symptoms
- Increasing drawing force
- Die wear
- Wire scratches
- Surface defects
- Higher wire temperature
- Shorter die life
Practical Solution
Check:
- Lubricant type
- Lubricant concentration
- Lubricant cleanliness
- Lubricant temperature
- Supply quantity
- Lubrication system condition
- Lubricant viscosity
The objective should be to maintain stable lubrication throughout production rather than correcting the problem only after wire defects appear.
4. Improper Die Alignment
Correct die alignment is particularly important in multi-pass and high-speed drawing operations.
If the die is not properly aligned with the wire path, the wire may not pass through the die concentrically.
This can create uneven loading on the die and lead to irregular wear.
Common Symptoms
- Uneven die wear
- Wire ovality
- Diameter variation
- Surface marks
- Increased vibration
Practical Solution
Check the complete wire path, including:
The die should be positioned correctly and securely so that the wire enters and exits without unnecessary lateral movement.
5. Incorrect Die Geometry
Die geometry has a significant influence on wire drawing performance.
Important geometric areas include:
- Approach angle
- Bearing length
- Reduction zone
- Back relief
- Entry and exit
An unsuitable geometry can increase friction, pressure, or unwanted contact with the wire.
Practical Solution
Die geometry should be selected according to the wire material, area of reduction, drawing speed, and application.
For critical applications, dimensional control of the die working zone is essential because even small geometry variations can affect drawing behaviour.
6. Damaged or Poor-Quality Incoming Wire
Sometimes the die is blamed for a problem that actually originates with the incoming wire.
Wire containing the following conditions can cause accelerated die wear or damage:
- Surface scale
- Scratches
- Dirt
- Oxidation
- Inconsistent diameter
- Excessive ovality
Hard particles or surface contamination can act as abrasives inside the drawing interface.
Practical Solution
Inspect the incoming wire before production.
Check:
- Wire diameter
- Ovality
- Surface condition
- Material consistency
Maintaining consistent incoming wire quality is an important part of protecting the drawing die.
7. Excessive Drawing Speed or Poor Thermal Control
Higher drawing speeds can increase frictional heating and place additional demands on the die and lubrication system.
If heat is not effectively controlled, thermal effects can contribute to accelerated wear and dimensional instability.
Practical Solution
Monitor:
- Drawing speed
- Lubricant temperature
- Cooling performance
- Wire temperature
- Die condition
If die life decreases significantly after increasing production speed, the complete process should be reviewed rather than assuming the die material is the only problem.
8. Using a Worn Die Beyond Its Effective Working Life
A die does not necessarily fail suddenly.
In many cases, deterioration happens gradually.
The working zone may wear while the wire continues to remain within the nominal diameter for some time. However, surface finish, ovality, dimensional stability, or production performance may already be deteriorating.
Warning Signs
- Increasing wire diameter variation
- Increasing ovality
- Surface scratches
- Increasing drawing force
- Visible wear in the working zone
- Frequent wire breaks
- Declining surface quality
Practical Solution
Instead of waiting for complete failure, establish inspection criteria based on production requirements.
Monitor die performance and replace or rework the die when it reaches the defined limit.
9. How Can Manufacturers Increase Wire Drawing Die Life?
Die life depends on the interaction of several factors rather than the die material alone.
A practical die-life improvement strategy should consider:
1. Select the Correct Die Material
Match the die material to the wire material, reduction, speed, and production requirement.
2. Control the Drawing Process
Maintain consistent reduction, speed, lubrication, and cooling conditions.
3. Maintain Accurate Alignment
Ensure that the wire enters and exits the die correctly.
4. Monitor Die Performance
Track diameter, ovality, surface finish, drawing force, and production quantity.
5. Maintain the Tooling
Clean, inspect, and rework dies using appropriate procedures.
6. Investigate Repeated Failures
If the same die position repeatedly fails, investigate the process rather than simply replacing the die.
10. TC, PCD or Diamond: Does Die Material Solve Everything?
Choosing the right die material is important, but die material alone does not determine die life.
A high-performance die can still experience premature wear if the process has:
- Poor lubrication
- Incorrect alignment
- Excessive reduction
- Contaminated wire
- Improper installation
- Excessive heat
- Poor maintenance
For this reason, die selection should always be considered together with the complete wire drawing process.
Depending on the application, manufacturers may consider Tungsten Carbide, PCD, Natural Diamond, or Synthetic Single Crystal Diamond tooling.
The appropriate choice depends on wire material, size range, drawing conditions, required surface quality, and expected production volume.
The correct die material is important, but stable process conditions are equally critical to achieving long die life.
A Simple Wire Drawing Die Troubleshooting Checklist
| Problem Observed | Possible Cause | What to Check |
|---|---|---|
| Rapid die wear | Lubrication / material / alignment | Lubrication, die material, wire path |
| Wire scratches | Die damage / contamination | Die working zone and wire cleanliness |
| Wire ovality | Alignment / uneven die wear | Die alignment and wear pattern |
| Diameter variation | Die wear / unstable process | Die dimensions and drawing conditions |
| Frequent wire breaks | Excessive reduction / die surface defects | Reduction schedule and incoming wire |
| Die cracking | Installation / excessive load | Die seating and drawing load |
| High drawing force | Lubrication / die geometry | Lubrication and die geometry |
| Poor surface finish | Die wear / contamination | Working zone and wire condition |
| Short die life | Process instability | Speed, lubrication, alignment, material |
| Repeated failure at same pass | Process-specific issue | Die position, reduction, and alignment |
Conclusion
Premature wire drawing die failure is rarely caused by one factor alone.
Die material, geometry, wire quality, lubrication, alignment, reduction, drawing speed, cooling, and maintenance all influence tooling performance.
The most effective approach is therefore not simply to replace a failed die, but to identify why it failed.
By monitoring die condition and controlling the complete drawing process, wire manufacturers can improve dimensional consistency, surface quality, production stability, and overall tooling efficiency.
The right die is only the beginning. The right process makes the difference.
About Mikrotek
Mikrotek manufactures precision wire drawing dies and tooling solutions for the wire and cable industry.
Our product portfolio includes:
- Natural Diamond Dies
- Synthetic Single Crystal Diamond Dies
- PCD Dies
- Tungsten Carbide Dies
- Diamond Coated Dies
- Enamelling Dies
- Taper Nibs
- Extrusion Tools
With application-focused tooling and die-working capabilities, Mikrotek supports wire manufacturers in selecting and maintaining the appropriate tooling for their production requirements.
Need Help Selecting the Right Wire Drawing Die?
Share your wire material, inlet diameter, outlet diameter, drawing speed, and application requirements with the Mikrotek team to discuss the appropriate tooling solution.
Frequently Asked Questions
1. Why does a wire drawing die wear out quickly?
Common causes include incorrect die material, excessive reduction, poor lubrication, improper alignment, contaminated wire, and unsuitable die geometry. The complete drawing conditions should be checked before simply replacing the die.
2. How can I increase the life of a wire drawing die?
Use the correct die material and geometry, maintain proper lubrication, control drawing speed and reduction, maintain accurate alignment, and regularly inspect and maintain the die.
3. What causes scratches on drawn wire?
Scratches can result from a worn or damaged die, contamination, poor incoming wire quality, or inadequate lubrication. Both the die working zone and incoming wire condition should be inspected.
4. What causes wire diameter variation and ovality?
Uneven die wear, improper alignment, inconsistent incoming wire dimensions, and unstable drawing conditions can cause diameter variation and ovality.
5. Does lubrication affect wire drawing die life?
Yes. Proper lubrication helps control friction and heat between the wire and die. Poor, contaminated, or insufficient lubrication can significantly increase wear and reduce die life.
6. When should a wire drawing die be replaced?
A die may need reworking or replacement when there is increasing diameter variation, ovality, surface damage, excessive working-zone wear, higher drawing force, declining surface quality, or frequent wire breaks.
